


EP Rubber Conveyor Belt
General Introduction:
EP rubber conveyor belt is widely used by the mining and processing industries for transporting bulk or lumpy materials such as quarrying, ore, coke, aggregates, crops, sand, clinker, chemicals, construction materials, etc.
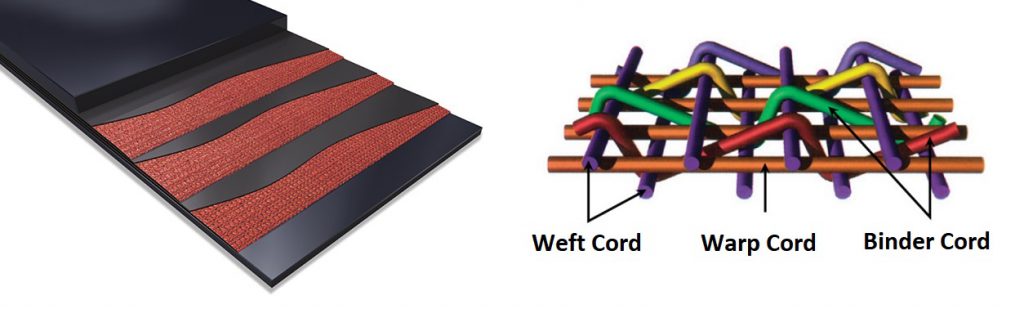
The EP is short for Polyester fabric, which includes polyester toward longitudinal(warp) and polyamide for latitude(weft), EP fabric plies are sandwiched between rubber skim coats for adhesion and load support. Bottom and top cover compounds are added for maximum protection of the belt carcass. The EP conveyor belt consisting of two to six EP fabric plies, EP rubber conveyor belt has the same merit as Nylon conveyor belt, in addition, EP fabric has the advantages of:
A.Lower longitudinal elongation.
B.Full resistance to mildew, moisture and rotting.
C.Good flexibility and trough ability.
D.Short take-up lengths.
E.Suitable for middle and long-distance transportation of higher load and speed.
The Top 5 Rubber Conveyor Belt Manufactures In China 2026
How to choose crushing plant conveyor belt for 100 ~ 1000T/H scale?
EP conveyor belt layer is the more the better?
How to choose the cover thickness of conveyor belt?
EP fabric also has excellent compatibility with other rubbers, so it can be combined with any type of cover grade to make it a perfect match for almost any application. This allows EP conveyor belt to convey basically any type of product in any environment, from fine powders to large lumps, from dry to greasy materials, from extremely cold to very hot conditions.
The common ep conveyor belt type could be:
2-ply belts: 315/2 400/2 500/2 630/2 800/2
3-ply belts: 500/3 630/3 800/3 1000/3 1250/3
4-ply belts: 630/4 800/4 1000/4 1250/4 1600/4
5-ply belts: 800/5 1000/5 1250/5 1600/5 2000/5
EP Fabric Technical Specification:
| Test Item | EP100 | EP125 | EP150 | EP200 | EP250 | EP300 | EP350 | EP400 | EP500 | |||||||||
| warp | weft | warp | weft | warp | weft | warp | weft | warp | weft | warp | weft | warp | weft | warp | weft | warp | weft | |
| Breaking strength (N/mm) | ≥100 | ≥55 | ≥125 | ≥65 | ≥150 | ≥75 | ≥200 | ≥78 | ≥250 | ≥80 | ≥300 | ≥80 | ≥350 | ≥75 | ≥400 | ≥90 | ≥500 | ≥105 |
| Breaking elongation (%) | ≥14.0 | ≤45.0 | ≥14.0 | ≤45.0 | ≥14.0 | ≤45.0 | ≥14.0 | ≤45.0 | ≥14.0 | ≤45.0 | ≥14.0 | ≤45.0 | ≥14.0 | ≤45.0 | ≥14.0 | ≤45.0 | ≥14.0 | ≤45.0 |
| Elongation at 10% load (%) | ≤1.5 | ≤1.5 | ≤1.5 | ≤1.5 | ≤1.5 | ≤1.5 | ≤1.5 | ≤2.0 | ≤2.0 | |||||||||
| Heat shrinkage (150℃, 30Min.) | ≤5.0 | ≤1.0 | ≤5.0 | ≤1.0 | ≤5.0 | ≤1.0 | ≤5.0 | ≤1.0 | ≤6.0 | ≤1.0 | ≤6.0 | ≤1.0 | ≤6.0 | ≤1.0 | ≤6.0 | ≤1.0 | ≤6.0 | ≤1.0 |
| Adhesion (N/2.5cm) | ≥196.0 | ≥196.0 | ≥196.0 | ≥196.0 | ≥196.0 | ≥196.0 | ≥196.0 | ≥196.0 | ≥196.0 | |||||||||
| Weight (G/m²) | 370±30 | 430±30 | 520±30 | 610±40 | 780±40 | 860±40 | 980±40 | 1180±50 | 1320±50 | |||||||||
| Thickness (mm) | 0.53±0.06 | 0.62±0.06 | 0.70 ± 0.06 | 0.85±0.09 | 1.00±0.10 | 1.15±0.10 | 1.20±0.10 | 1.50±0.12 | 1.70±0.14 | |||||||||
SUNGDA EP rubber conveyor belt products have five types according to coating difference: Anti-split type, Anti-abrasion type, common type,acid-alkali resistant type, and heat-resistant conveyor belt type.
Cover Rubber Grade for EP Conveyor Belt:
DIN22102 Standard:
| Standard | DIN-W | DIN-X | DIN-Y | DIN-Z | ||
| Tensile test | Before Aging | Tensile Strength (Mpa) | >18 | >25 | >20 | >15 |
| Elongation(%) | >400 | >450 | >400 | >350 | ||
| After Aging | Change rate of TS(%) | ±25 | ±25 | ±25 | ±25 | |
| Change rate of EL(%) | ±25 | ±25 | ±25 | ±25 | ||
| Abrasion test(mm³) | <90 | <120 | <150 | <250 | ||
AS-RMA Standard
| Standard | AS-N | AS-M | AS-A | RMA-I | RMA-II | ||
| Tensile test | Before Aging | Tensile Strength (Mpa) | >17 | >24 | >17 | >17 | >14 |
| Elongation(%) | >400 | >450 | >400 | >450 | >400 | ||
| After Aging | Change rate of TS(%) | ±20 | ±20 | ±20 | ±25 | ±25 | |
| Change rate of EL(%) | ±20 | ±20 | ±20 | ±25 | ±25 | ||
| Abrasion test(mm³) | <200 | <125 | <70 | <150 | <200 | ||
-
DIN-W, AS-A & AS-M (High Wear Resistance): Feature superior abrasion resistance (DIN-W <90 mm³, AS-A <70 mm³, AS-M <125 mm³) and high tensile strength. Ideal for severe impact and high-wear environments handling sharp, highly abrasive bulk materials (e.g., hard rock, iron ore, and heavy aggregates) across long-distance, high-capacity mining and quarrying conveyors.
-
DIN-X & RMA-I (General Heavy Duty): Offer balanced cut and gouge resistance with moderate abrasion loss (<120 mm³ and <150 mm³). Suited for primary and secondary crushing plants, steel mills, and coal handling facilities transporting large lump sizes and heavy tonnages over medium-to-long distances.
-
DIN-Y, DIN-Z, AS-N & RMA-II (General Service): Designed for standard conditions with higher abrasion values (<150 to <250 mm³). Best applied in light-to-moderate industrial transport systems, sand, and agricultural facilities moving fine-to-medium sized, non-abrasive materials with low impact stress over shorter distances.
Muti-ply EP Fabric Grade (Tensile Strength kg/cm, PIW):
| Fabric/Ply | 3P | 4P | 5P | 6P | ||||
| kg/cm | PIW | kg/cm | PIW | kg/cm | PIW | kg/cm | PIW | |
| EP-100 | 300 | 1680 | 400 | 2240 | 500 | 2800 | 600 | 3360 |
| EP-125 | 375 | 2100 | 500 | 2800 | 625 | 3500 | 750 | 4200 |
| EP-150 | 450 | 2520 | 600 | 3360 | 750 | 4200 | 900 | 5040 |
| EP-200 | 600 | 3360 | 800 | 4480 | 1000 | 5600 | 1200 | 6720 |
| EP-250 | 750 | 4200 | 1000 | 5600 | 1250 | 7000 | 1500 | 8400 |
| EP-300 | 900 | 5040 | 1200 | 6720 | 1500 | 8400 | 1800 | 10080 |
| EP-350 | 1050 | 5880 | 1400 | 7840 | 1750 | 9800 | 2100 | 11760 |
* PIW=Pounds Per Inch Of Belt Width
If you are from the U.S or Europe, you may need to convert between PIW with N/mm, please click here to see how to convert it.
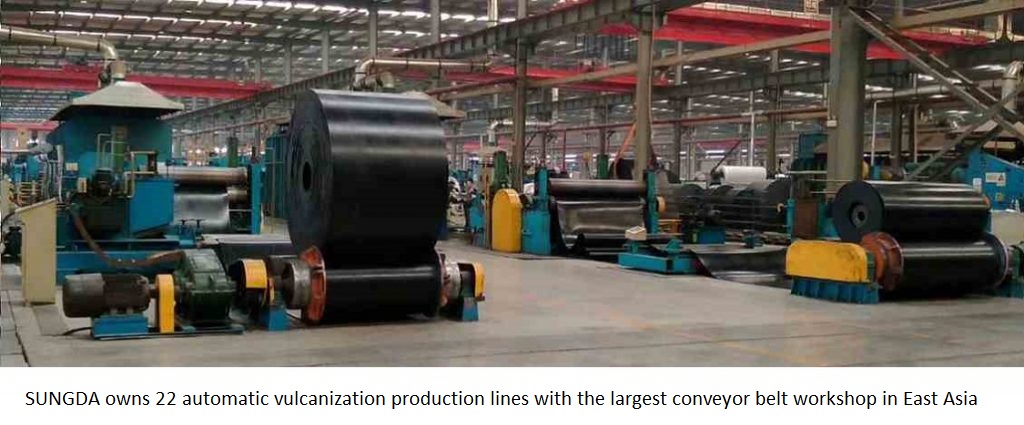
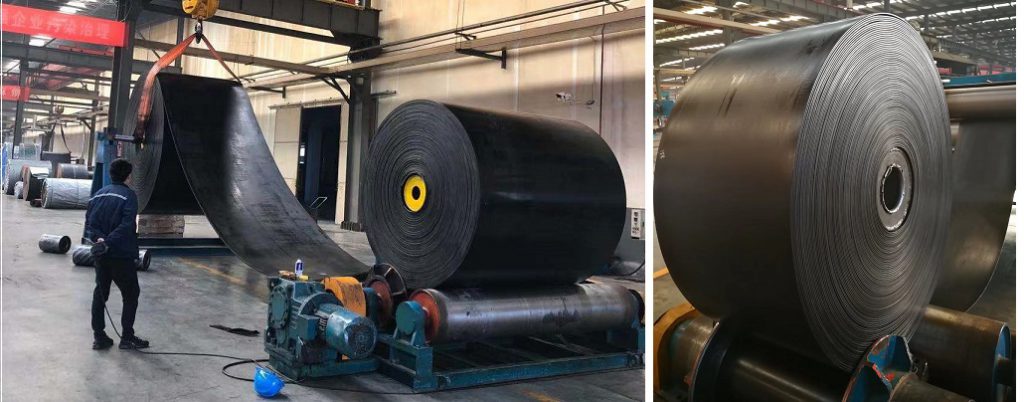
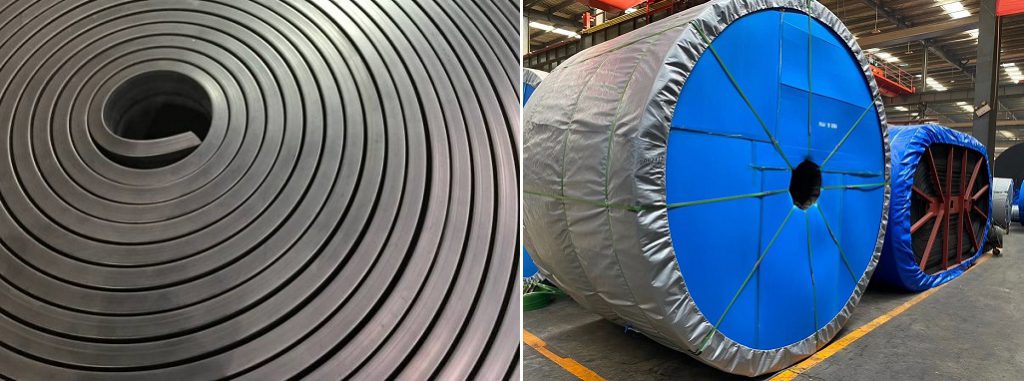
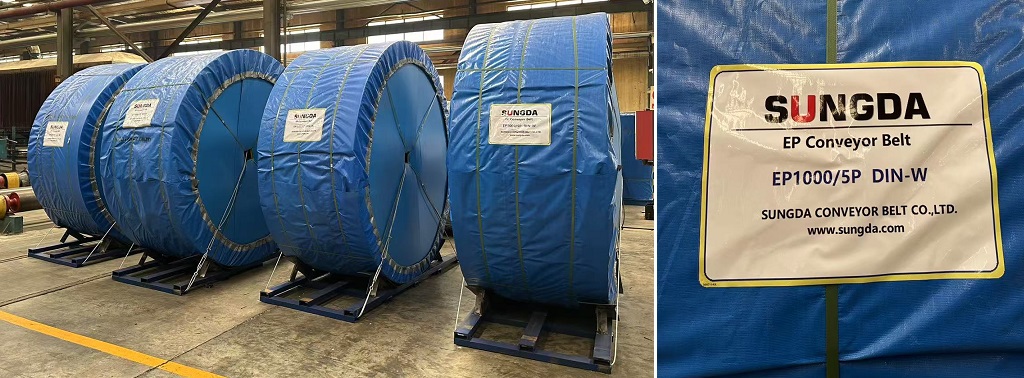
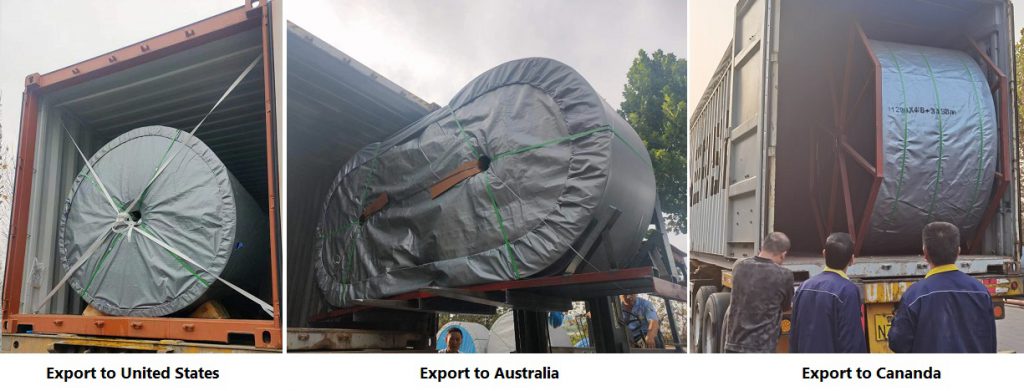
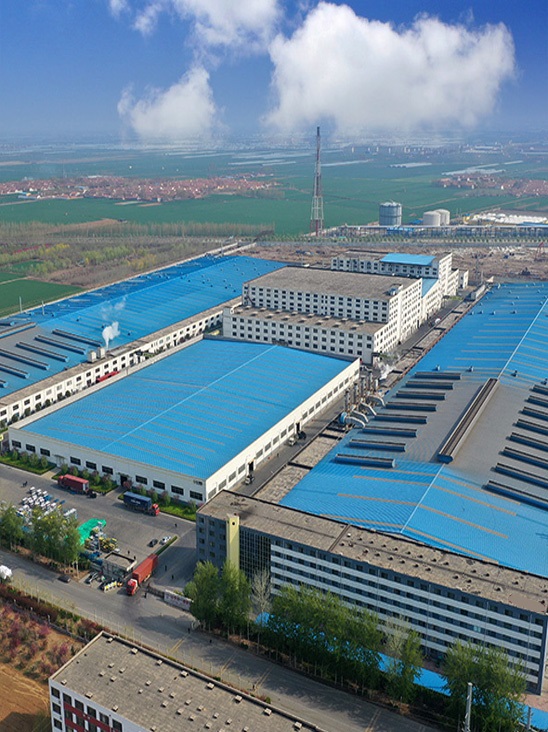
SUNGDA Conveyor Belt Vulcanization Workshop
Related Ep conveyor belt article:
-
What are the advantages of EP conveyor belts compared to ordinary conveyors?
-
How does the bending of EP fabric affect the working life of the conveyor belt?
-
What is PIW in the EP conveyor belt and how to convert it into N/mm
-
How to identify the quality of the EP conveyor belt in one minute?
10 Technical FAQs About Fabric (EP) Conveyor Belts for Heavy-Duty Conveying
1. How do I accurately calculate the required EP belt tension rating (EP Grade)?
Unlike steel cord belts, fabric belts are designated by their total carcass nominal breaking strength across all plies (e.g., an EP800/4 belt consists of 4 plies, each rated at 200 N/mm, yielding a total nominal breaking strength of 800 N/mm).
Selecting the correct EP grade requires evaluating the maximum belt tension (Tmax) under steady-state operating conditions and dynamic transients (starting and stopping):
Required Nominal Belt Strength (EP)≥Tmax /W x S0
(Where Tmax is the maximum belt tension in kN, W is belt width in meters, and S0 is the safety factor).
For multi-ply fabric belts, static and dynamic safety factors (S0) typically range from 10:1 to 12:1 under standard CEMA / DIN 22102 design rules to account for ply-to-ply load distribution variations and mechanical fastener or vulcanized splice efficiency.
Typical DIN/ISO-Type Fabric Belt Specifications:
| EP Designation | Number of Plies | Individual Ply Rating | Total Nominal Strength | Max Recommended Working Tension (Tperm)* |
| EP400/3 | 3 | 133 N/mm | 400 N/mm | ~40 N/mm |
| EP500/4 | 4 | 125 N/mm | 500 N/mm | ~50 N/mm |
| EP630/4 | 4 | 157 N/mm | 630 N/mm | ~63 N/mm |
| EP800/4 | 4 | 200 N/mm | 800 N/mm | ~80 N/mm |
| EP1000/5 | 5 | 200 N/mm | 1,000 N/mm | ~100 N/mm |
| EP1250/5 | 5 | 250 N/mm | 1,250 N/mm | ~125 N/mm |
*Based on a standard 10:1 working safety factor; actual allowable tension varies depending on joint type (vulcanized vs. mechanical).
2. What makes EP (Polyester/Polyamide) superior to NN (Nylon/Nylon) fabric belts?
Understanding fabric composition is essential for avoiding premature belt stretch and tracking failures:
Warp Fabric (Polyester / E): Runs longitudinally along the conveyor length. Polyester provides an exceptionally low dynamic elongation (typically <1.5% at nominal working load), which drastically reduces take-up stroke requirements compared to Nylon warp fabric.
Weft Fabric (Polyamide / P): Runs transversely across the belt width. Polyamide (Nylon) provides superior transverse flexibility, impact resistance, and mechanical fastener retention.
Compared to NN belts (Nylon warp and weft), EP belts exhibit lower operational stretch, higher resistance to moisture and mold, and superior thermal stability, making them the industry standard for medium-to-long distance bulk material handling.
3. Is more plies always better for heavy-duty applications?
No. Increasing the number of plies adds total tensile strength, but over-plying causes severe mechanical disadvantages:
1.Reduced Troughability: Excessively thick, multi-ply belts become overly stiff across their width, preventing proper contact with the center idler when empty and leading to severe mistracking.
2.Increased Minimum Pulley Diameters: Additional plies increase the total carcass thickness (e), raising inter-ply shear stress during bending. An EP1000/5 belt requires significantly larger pulleys than an EP1000/3 belt to prevent ply separation.
3.Higher Bending Fatigue: Repeated flexure over small drive pulleys causes inter-ply delamination over time.
Engineering best practice dictates choosing fewer plies with higher individual ply ratings (e.g., EP800/3 instead of EP800/5) to maximize troughability and reduce bending stress.
4. What is the realistic service life expectation for an EP conveyor belt?
Engineering life assessments must decouple Carcass Fatigue Life from Cover Rubber Wear Life:
EP Fabric Carcass: Under normal continuous operation, an EP carcass is engineered for a 5 to 10-year fatigue design life. Unlike steel cords, synthetic fibers experience gradual flexural fatigue and moisture aging.
Top/Bottom Covers: Cover wear is governed by material lump size, sharp edges, drop height at transfer points, and loading frequency. In heavy mining or aggregate crushing, top covers may wear down in 2 ~ 4 years, requiring cold-bonding repair or re-covering while the EP core remains structurally sound.
5. What are the key troughability and pulley diameter limits for EP belts?
Belt troughability must be verified against idler angle (20℃, 35℃, or 45℃) to ensure the unladen belt molds into the idler trough. Minimum drive pulley diameters (DA) per DIN 22102 are governed by total carcass thickness and stress levels:
| EP Designation | Carcass Thickness (Approx.) | Min. Drive Pulley DA (100% Load) | Min. Troughability Width (35∘ Idlers) |
| EP400/3 | ~3.6 mm | 315 mm | 500 mm |
| EP630/4 | ~4.8 mm | 400 mm | 650 mm |
| EP800/4 | ~5.2 mm | 500 mm | 800 mm |
| EP1000/5 | ~6.5 mm | 630 mm | 1,000 mm |
| EP1250/5 | ~7.2 mm | 800 mm | 1,200 mm |
Procurement Warning: Installing an EP1000/5 belt on a system designed with 400 mm pulleys will cause rapid inter-ply delamination within months of commissioning.
6. Hot Vulcanized, Cold Bonded, or Fastened: Which splice method should be specified?
The choice of joint method directly determines allowable working tension and system reliability:
Hot Vulcanized Splices (Efficiency: 85% – 90%): The gold standard for permanent installations. Uses step-matching ply techniques under heat and pressure. Required for high-tension EP belts (≥EP630).
Cold Bonded Splices (Efficiency: 70% – 80%): Uses specialized two-part cement at ambient temperatures. Ideal for underground or hazardous locations where hot vulcanizing presses cannot be operated.
Mechanical Fasteners (Efficiency: 50% – 65%): Plate or wire-hook fasteners offer rapid repair times but create stress concentrations and wear out scrapers. Recommended only for temporary applications, low-tension short runs, or emergency repairs.
7. How do I select the right cover rubber grade (DIN 22102 / ISO 10247)?
The rubber cover protects the load-bearing EP carcass from impact, abrasion, and environmental degradation. Standard cover grades are categorized by mechanical properties:
Grade W (ISO ‘D’): Premium abrasion resistance (≤90mm3loss). Recommended for highly abrasive materials like quartz, iron ore, and heavy sinter.
Grade X (ISO ‘H’): Balanced high abrasion and cut/gouge resistance (≤120mm3 loss). Ideal for large lump limestone, granite, and sharp metallic ores.
Grade Y (ISO ‘L’): Standard duty abrasion resistance (≤150mm3 loss). Suited for coal, sand, gravel, and general bulk materials.
Special Duty Compounds: Heat-resistant (HR / HRT up to 200°C), Oil-resistant (OR), and Flame-retardant (FR) formulations must be specified if chemical, thermal, or underground safety criteria apply.
8. What causes ply delamination, and how can it be prevented during procurement?
Ply delamination—the separation of adjacent fabric plies—is the leading cause of premature fabric belt failure. It is caused by:
Insufficient Inter-Ply Adhesion Strength: Low rubber-to-fabric bond strength during manufacturing.
Excessive Bending Stress: Running the belt over undersized pulleys or reverse bends.
Because synthetic fabrics exhibit higher elastic and permanent elongation than steel cords, gravity or hydraulic take-up units require significantly longer travel distance:
Chemical / Oil Ingress: Hydrocarbons or chemicals penetrating edge cuts and dissolving the skim rubber layer.
Procurement Rule: Always specify Inter-Ply Peel Strength ≥4.5N/mm (per ISO 252 testing) and ensure full rubber-sealed edges (Molded Edges rather than Cut Edges) for wet or chemically aggressive environments.
9. How does take-up travel calculation differ between EP belts and steel cord belts?
Take-Up Travel Allowance≈1.5%~ 2.5%) x Conveyor Center Distance
EP Belts: Require approximately 1.5~2.0% of total center distance in take-up stroke (e.g., a 200 m conveyor needs 3.0~4.0m of take-up travel).
Comparison with NN Belts: NN belts require up to 3.5% ~ 4.0% travel stroke, whereas Steel Cord belts require only 0.2% ~ 0.5%.
If take-up space is physically constrained on an existing structure, retrofitting from NN to EP—or specifying a high-modulus low-stretch EP weave—is mandatory to prevent take-up carriage bottoming out.
10. How should condition monitoring be conducted on fabric EP conveyor belts?
Unlike steel cord belts, which rely on electromagnetic scanners, multi-ply EP belts require a combination of visual, mechanical, and ultrasonic diagnostics:
Cover Thickness Ultrasonic Profiling: Non-destructive ultrasonic gauges measure remaining top and bottom cover rubber over time to schedule re-topping or replacement.
Visual & Thermographic Joint Monitoring: Infrared cameras detect anomalous heat buildup at splices caused by internal ply friction or dynamic joint slip prior to separation.
Automated Edge Inspection: Optical sensors monitor edge wear and ply fraying caused by structure rubbing, catching tracking issues before moisture penetrates the internal carcass.
Transitioning from time-based replacement to state-of-the-art condition-based monitoring ensures maximum tonnage throughput while eliminating catastrophic carcass snaps.
Specifications for Conveyor Belt Rubber Covers Across Countries and Regions
| Cover Grade | Country | Applicable Standards | Min.Tensile Strength(Mpa) | Min.Elongation at Break(%) | Max.Abrasion Loss(mm3) |
| DIN-Z | Germany | DIN22102 | 15 | 350 | 250 |
| DIN-Y | Germany | DIN22102 | 20 | 400 | 150 |
| DIN-X | Germany | DIN22102 | 25 | 450 | 120 |
| DIN-W | Germany | DIN22102 | 18 | 400 | 90 |
| RMA-I | U.S.A | RMA | 17 | 400 | 150 |
| RMA-II | U.S.A | RMA | 14 | 400 | 200 |
| ARPM RMA-I | U.S.A | ARPM | 17 | 400 | 125 |
| ARPM RMA-II | U.S.A | ARPM | 14 | 400 | 175 |
| ISO-L | International | ISO -10247 | 15 | 350 | 200 |
| ISO-H | International | ISO -10247 | 24 | 450 | 120 |
| ISO-D | International | ISO -10247 | 18 | 400 | 100 |
| AS-N | Australian | AS -1332 | 17 | 400 | 200 |
| AS-M | Australian | AS -1332 | 24 | 450 | 125 |
| AS-A | Australian | AS -1332 | 17 | 400 | 70 |
| SANS-N | South Africa | SANS-1173 | 17 | 400 | 150 |
| SANS-M | South Africa | SANS-1173 | 25 | 450 | 120 |
| SANS-A | South Africa | SANS-1173 | 18 | 400 | 70 |
| BS-M | UK | BS-490 | 24 | 450 | 120 |
| BS-N | UK | BS-490 | 17 | 400 | 200 |
| IS-N-17 | India | IS 1891 | 17 | 400 | 200 |
| IS-M-24 | India | IS 1891 | 24 | 450 | 150 |
| JIS-G | Japan | JIS-K 6332 | 14 | 400 | 250 |
| JIS-L | Japan | JIS-K 6332 | 15 | 350 | 200 |
| JIS-D | Japan | JIS-K 6332 | 18 | 400 | 100 |
| JIS-H | Japan | JIS-K 6332 | 24 | 450 | 120 |
| GB-H | China | GB/T 7984 | 24 | 450 | 120 |
| GB-D | China | GB/T 7984 | 18 | 400 | 100 |
| GB-L | China | GB/T 7984 | 15 | 350 | 200 |
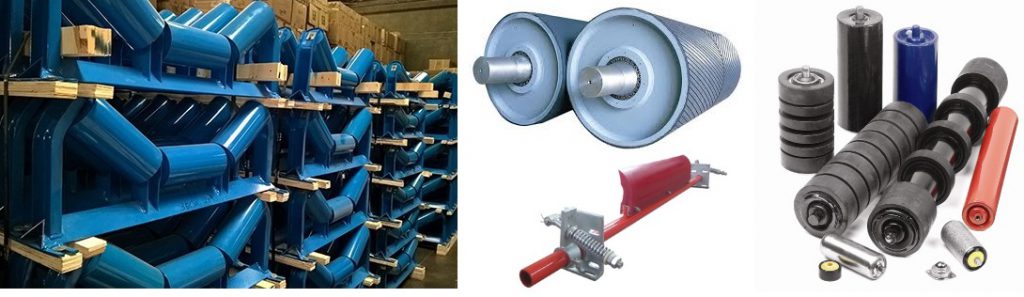
We also supply conveyor idlers, pulleys and conveyor brackets, please log on our brach company www.conveyoroller.com for more information.
Tags: Abrasion resistance of EP conveyor belts,Advantages and features of EP conveyor belts,aggregate ep conveyor belt,anti-static properties of ep conveyor belt,Applications and industries of EP conveyor belts,Bulk material ep conveyor belt,Buying guide for EP conveyor belts,Cement ep conveyor belt,Chemical resistance of ep conveyor belt,Chemical resistance of EP conveyor belts,coal ep conveyor belt,Comparison of EP conveyor belts with other types,crushing plant ep conveyor belt,Ep conveyor belt specification,Ep fabric conveyor belt,EP rubber conveyor belt,ep1000/3 conveyor belt,ep1000/5 conveyor belt,ep1250 conveyor belt,ep1250/4 conveyor belt,ep1250/5 conveyor belt,ep160 conveyor belt,ep250 conveyor belt,ep315/2 conveyor belt,ep315/3 conveyor belt,ep400 conveyor belt,ep400/3 conveyor belt,ep630 conveyor belt,EP630/4 conveyor belt,ep800/3 conveyor belt,ep800/4 conveyor belt,ep800/5 conveyor belt,Installation and commissioning tips for ep conveyor belt,internation standards for ep conveyor belt,International standards and certifications for EP conveyor belts,Maintenance and care for EP conveyor belts,Manufacturers of EP conveyor belts,mining EP conveyor belt,polyester conveyor belt,Pricing and cost of EP conveyor belts,quarry ep conveyor belt,Reliability and durability of EP conveyor belts,Rubber conveyor belt,steel plant ep conveyor belt,Temperature range for EP conveyor belts,tensile strength of ep conveyor belt,Tensile strength of EP conveyor belts,Waterproof properties of EP conveyor belts
Related Products
-
Material Composition of High-Quality Conveyor Belts (from ContiTech & Dunlop)
No. -
What are the Basic Indicators that Determine the Quality of Conveyor Belts?
No. -
What Are the Tensile Strength and Elongation in Rubber Conveyor Belts?
No. -
What’s “kg/cm²” in Conveyor Belt and How Convert it into other Units?
No. -
What is the difference between PSI and Mpa in conveyor belts and how to convert them to each other?
No. -
How to conduct conveyor belt troughing test
No. -
The Most Comprehensive National and Organizational Conveyor Belt Testing Standards
No. -
What are the chemical properties of various rubber components in rubber conveyor belts?
No. -
How to reasonably design long-distance conveyor lines
No. -
The 4 most critical tips for choosing the right rubber conveyor belt
No.