


Steel Cord Conveyor Belt
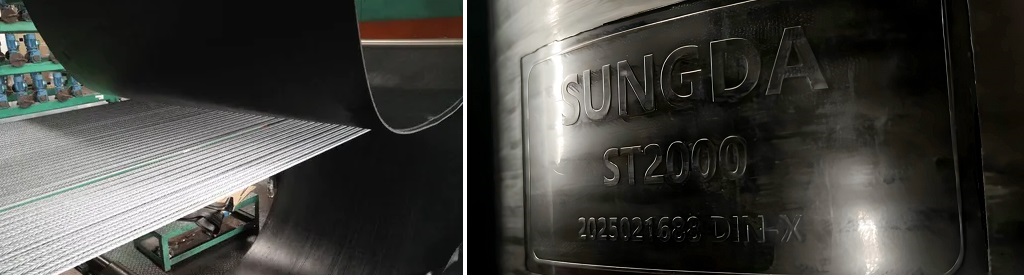
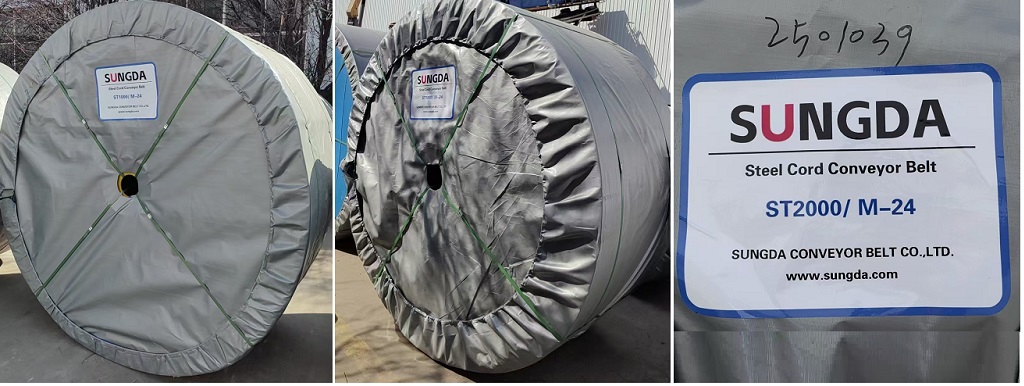
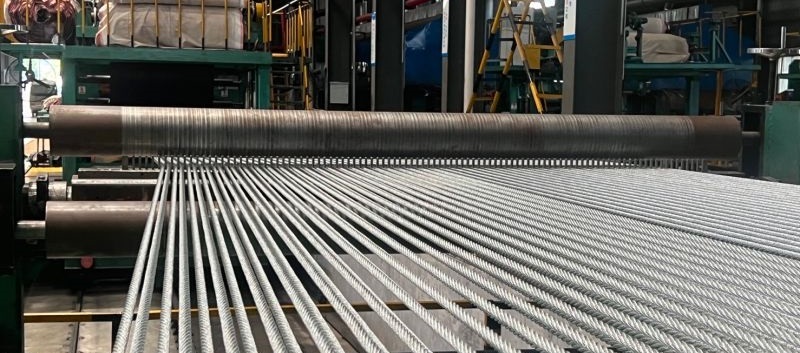
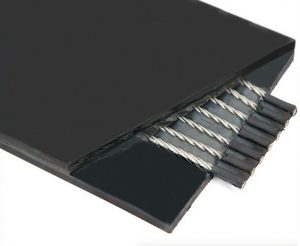
The steel cord conveyor belt consists of steel cord (ST800/ST1000/ST1250/ST1400/ST1600/ST1800/ST2000/ST2250 etc.) and rubber covering,the production process includes steps such as steel cord weaving, rubber mixing, extrusion and vulcanization. Compared with EP conveyor belts, steel cord conveyor belts have higher tensile strength, abrasion resistance and corrosion resistance, more importantly, due to the super tensile strength of steel cords, they overcome the problems of easy deformation and overstretching of EP conveyor belts, so it is more suitable for long-distance, heavy-duty and high-speed transportation, widely used in mining industry, steel mill, seaports, building materials, metallurgy and other industries, especially in harsh environments and high-intensity working conditions.
Characteristics:
1. High tensile strength: The belts are suitable for large span, long-distance transportation of materials.
2. Small elongation in use: The belts need only a very short take-up stroke distance.
3. The small diameter of drive pulley: The belt body has a layer of longitudinally arranged steel cords as its skeleton, and thus is resistant to flex fatigue. Therefore, a drive pulley of smaller diameter can be used to make the equipment smaller.
4. High adhesion between rubber and steel cord: The steel cords are coated with zinc on their surface, and also the rubber used has the property of good adhesion with steel cords. Therefore, the rubber is tightly adhered to the steel cords and is resistant to shock and difficult to drop, so the rubber belts are long in life.
5. Even tension of steel cords: Because of advanced techniques in manufacturing, the steel cords are very evenly arranged and have the same tension, so the belts are well-balanced in running and difficult to run awry.
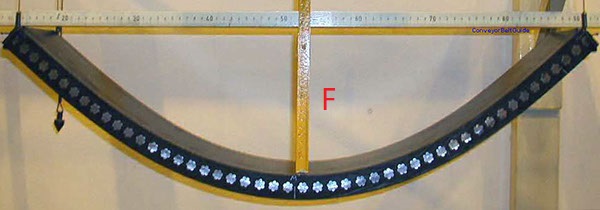
6. Good trough ability: As the belt body has no transverse skeleton, it is easy to form a deep trough, so the belts can load more materials and prevent the materials from escaping.
7. Inspection of the belt with X-rays: Users can use X-rays to inspect damages of the skeleton steel cords on the conveyor machines to prevent accidents from happening.
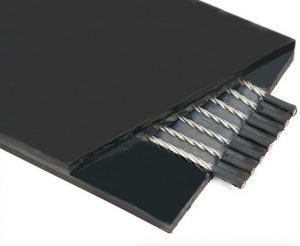
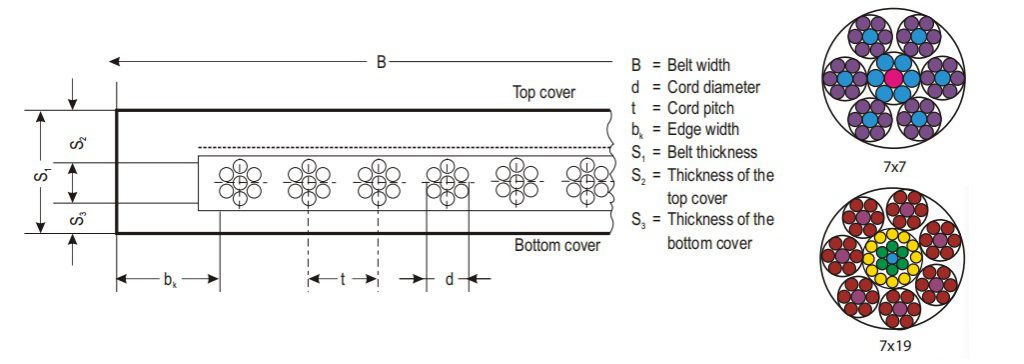
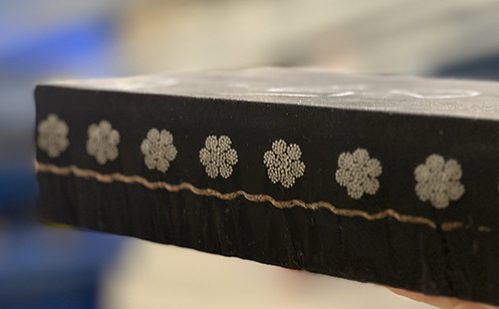
Steel Cord Conveyor Belt Carcass:
Steel cord conveyor belt’s key to symbol:
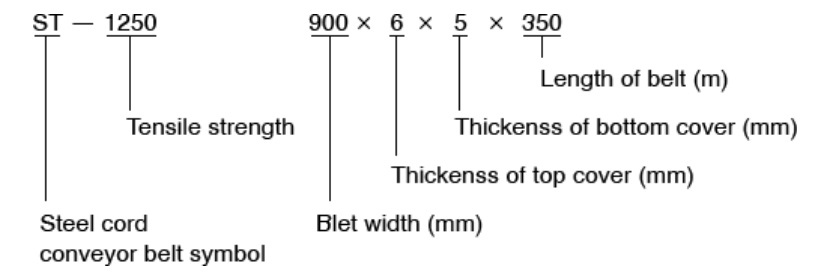
Steel cord conveyor belt specification:
Strength grade | Tensile strength (N/mm) | Steel Cord pitch (mm) | Steel Cord diameter (mm) | Min.breaking force (KN) | Min.cover thickness (mm) |
ST-500 | 500 | 10 | 2.5 | 5.5 | 4 |
ST-630 | 630 | 10 | 2.8 | 7 | 4 |
ST-800 | 800 | 10 | 3 | 8.9 | 4 |
ST-1000 | 1000 | 12 | 3.4 | 12.9 | 4 |
ST-1250 | 1250 | 12 | 3.8 | 16.1 | 4 |
ST-1400 | 1400 | 12 | 4.3 | 18 | 4 |
ST-1600 | 1600 | 12 | 4.7 | 20.6 | 4 |
ST-2000 | 2000 | 12 | 5.0 | 25.6 | 4 |
ST-2250 | 2250 | 12 | 6.6 | 29 | 4 |
ST-2500 | 2500 | 15 | 6.8 | 40 | 5 |
ST-2800 | 2800 | 15 | 7 | 44.8 | 5 |
ST-3150 | 3150 | 15 | 7.3 | 50.5 | 5.5 |
ST-3500 | 3500 | 15 | 8.2 | 56 | 6 |
ST-4000 | 4000 | 15 | 8.8 | 63.5 | 6.5 |
ST-4500 | 4500 | 16 | 9.7 | 76.3 | 7 |
ST-5000 | 5000 | 17 | 10.9 | 91 | 7.5 |
ST-5400 | 5400 | 17 | 11.3 | 98.2 | 8 |
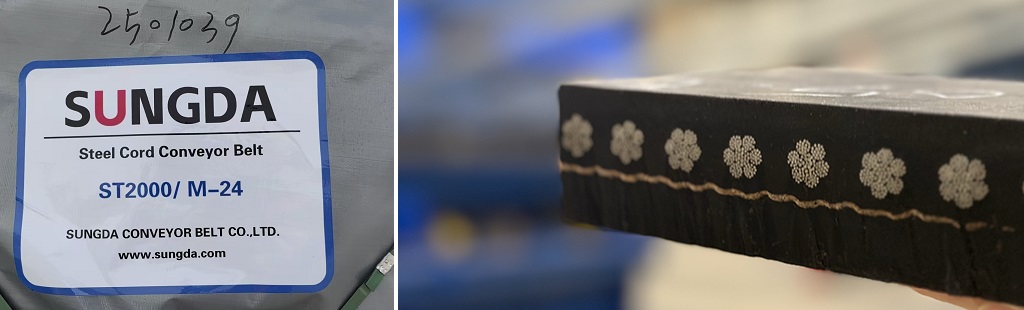
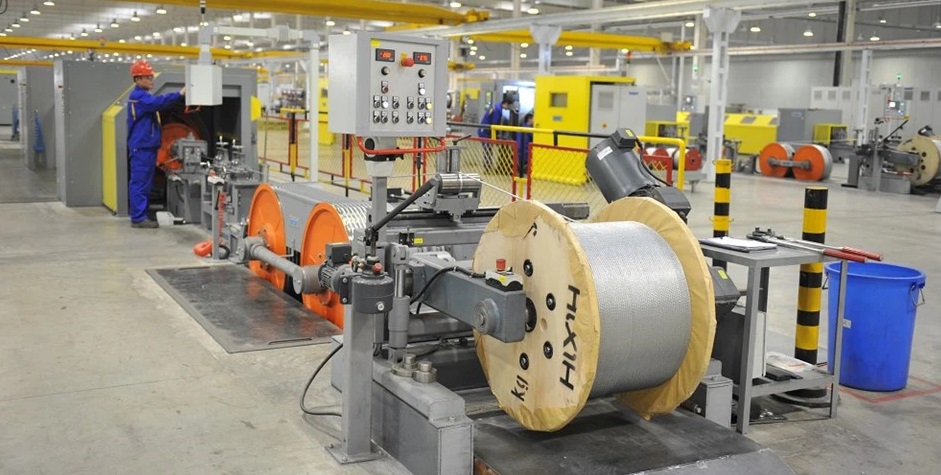
Steel cord is the core component of steel cord conveyor belts, providing the strength and stability necessary to withstand high tension and repeated pulling forces. SUNGDA’s steel cord utilizes Contitech’s specialized “HIXIH” brand high-strength steel cord, enabling SUNGDA’s series of steel cord conveyor belts to meet the demands of long-distance, high-strength, and various adverse operating conditions. The steel cord has the following advantages:
1.Zinc Galvanized and High Tension Open Type Steel Cord
Sungda selects its cord construction to provide the best specifications for particular applications. The cords are constructed to offer high flexibility, low elongation, and efficient, high-strength splice designs. The galvanized zinc coating serves as a bonding agent between the steel cord and skim rubber, providing a crucial barrier against corrosion.
2.Limited Take-up Travel
Sungda belts elongate a maximum of 0.25% at rated tension. This allows for lower-cost take-up systems on many applications, making Sungda the preferred choice for long overland and short stacker/reclaiming systems where minimum elongation is critical.
3.Long Splice Life:
Our proven splicing methods, validated by dynamic splice testers, result in dynamic splice efficiencies exceeding the 50% rating defined in DIN 22131 Part 3. With proper technique, splices on Sungda belts should last the life of the belt.
4.High Impact Resistance
Advanced cover compounds and skim rubber with superior adhesion combine to provide the impact, tear, and rip resistance demanded by your applications.
5.Lower Cost-per-Ton
Fewer conveyors and splices, shorter take-ups, and reduced belt inventory lead to longer belt life, longer splice life, and reduced downtime. All these factors contribute to a lower cost-per-ton of material conveyed, making a significant improvement in your bottom line.
Steel Cord Conveyor Belt Specification(PIW):
| Type | Minimum UItimate Tension (PIW) | Operating Tension (PIW) | Cable Diameter (in) | Cable Pitch (in) | Belt Modulus (PIW) |
| ST800 | 4568 | 685 | 0.142 | 0.688 | 329000 |
| ST1000 | 5710 | 856 | 0.142 | 0.547 | 411000 |
| ST1250 | 7138 | 1070 | 0.205 | 0.855 | 514000 |
| ST1600 | 9136 | 1370 | 0.205 | 0.666 | 657000 |
| ST2000 | 11420 | 1712 | 0.205 | 0.533 | 822000 |
| ST2500 | 14275 | 2140 | 0.205 | 0.450 | 1030000 |
| ST3150 | 17987 | 2697 | 0.315 | 0.768 | 1290000 |
| ST3500 | 19985 | 2996 | 0.315 | 0.690 | 1440000 |
| ST4000 | 22840 | 3424 | 0.362 | 0.792 | 1640000 |
| ST4500 | 25695 | 3852 | 0.394 | 0.805 | 1850000 |
| ST5000 | 28550 | 4280 | 0.433 | 1.098 | 2050000 |
| ST5400 | 30835 | 4623 | 0.433 | 1.023 | 2220000 |
Steel Cord Conveyor Belt’s Cover Grade:
| Rubber Cover Type | Characterization | Tensile Strength in Mpa(min) | Elongation at break %(min) | Abrasion in mm³ (max) | Hardness in SHA | Basic Material |
| DIN – X | Extreme abrasion resistance,superior resistance to cutting & tearing | 25 | 450 | 120 | 60±5 | NR/SBR |
| DIN – Y | Excellent Impact and abrasion resistance | 20 | 400 | 150 | 60±5 | NR/SBR |
| DIN – W | Good abrasion resistance,superior resistance to cutting & tearing | 18 | 400 | 90 | 60±5 | NR/SBR |
| DIN – Z | Normal abrasion resistance and cutting & tearing resistance | 15 | 350 | 250 | 60±5 | NR/SBR |
| DIN – K | Flame Retardant (M HSA) | 15 | 350 | 200 | 60±5 | CR |
| G | Oil Resistant | 15 | 400 | 200 | 60±5 | NBR |
| C | Chemical Resistant | 15 | 400 | 250 | 60±5 | CR/IIR |
| E | Anti-Static | 15 | 400 | 200 | 60±5 | NR/SBR |
| HR | Heat Resistant+100℃~+175℃ | 15 | 400 | 200 | 60±5 | SBR/EPDM |
| RMA – I | High abrasion resistance,superior resistance to cutting &tearing | 17 | 450 | 200 | 60±5 | NR/SBR |
| RMA – II | Resistant to cuts and gouges, flexible at lower temperatures | 14 | 400 | 250 | 60±5 | NR/SBR |
TRF(transverse reinforcing fabric) type
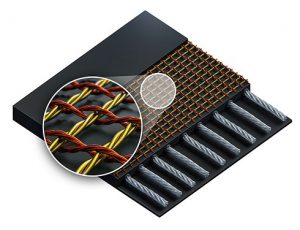
The feature of TRF type:
Prevention of longitudinal split or tear caused by hard materials or large objects with sharp edges.
Prevention of standing(jumping-out) of broken steel cords.
Less drop in pull-out force due to impact.
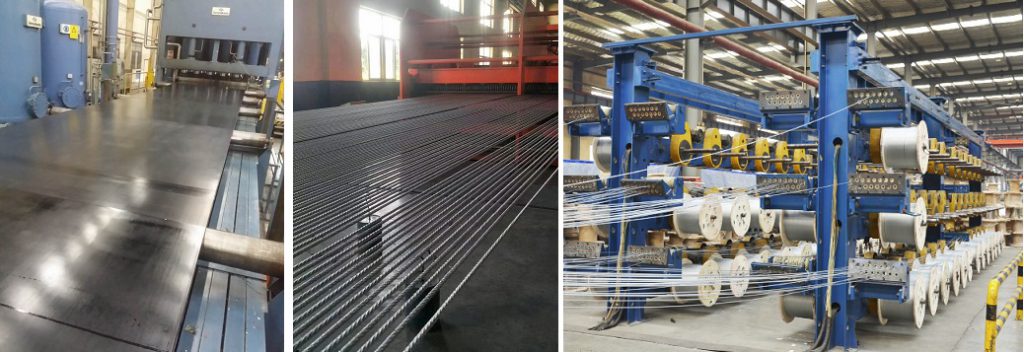
Compared with EP conveyor belts, steel cord conveyor belts are more complicated in the manufacturing process, which is mainly due to the following three reasons:
Steel cord rope weaving: The core of the steel wire rope conveyor belt is made of multi-layer steel cord rope weaving, manufacturers are required to master professional weaving technology to ensure the tight connection and uniform distribution of steel wires.
Rubber extrusion: The steel cord core needs to be covered by rubber, which requires rubber mixing and extrusion technology, manufacturers need to master the reasonable formula and extrusion process of rubber to ensure the uniformity and adhesion of the rubber covering layer.
Forming and vulcanization of the conveyor belt:The forming process requires equipment that can combine the steel cord core with the rubber covering layer well to form a strong conveyor belt structure, the vulcanization process requires control of parameters such as temperature, pressure and time to ensure that the tape achieves the desired physical properties.
Since the manufacturing process of the steel cord conveyor belt is more complicated, the manufacturer is required to have very strong technical strength and a more advanced vulcanization production line, and have strict quality control processes before, during and after production, only advanced equipment and professional With a professional technical team, the man
10 Technical FAQs About Steel Cord Conveyor Belts
1. How do I determine the required steel cord conveyor belt strength (ST Rating)?
The belt strength rating (ST rating) should be derived from the maximum calculated belt tension under both steady-state and dynamic (starting/stopping) transient conditions, rather than selected simply based on conveyor length or belt width.
Required Nominal Belt Strength (ST)≥(Tmax/W)x S0
(Where Tmax is the maximum belt tension in kN, W is belt width in meters, and S0 is the dynamic safety factor).
Modern overland conveyors equipped with soft-starters, variable frequency drives (VFDs), and controlled braking can reduce the dynamic safety factor S0 from traditional values (6.7 ~ 9.0) to 4.5 ~ 5.0 or lower under dynamic simulation analysis (e.g., CEMA / DIN 22101).
Typical ISO-Type Technical Reference:
| ST Grade | Nominal Strength | Cord Diameter | Cord Pitch | Allowable Working Tension (Tperm)* |
| ST1000 | 1,000 N/mm | ~4.0 mm | 12 mm | ~140 N/mm |
| ST1600 | 1,600 N/mm | ~5.0 mm | 12 mm | ~225 N/mm |
| ST2500 | 2,500 N/mm | ~7.5 mm | 15 mm | ~355 N/mm |
| ST3150 | 3,150 N/mm | ~8.1 mm | 15 mm | ~450 N/mm |
| ST4000 | 4,000 N/mm | ~9.1 mm | 17 mm | ~570 N/mm |
| ST5400 | 5,400 N/mm | ~11.3 mm | 17 mm | ~760 N/mm |
*Representative standard data; actual allowable working tension must account for dynamic splice efficiency and conveyor dynamics.
2. What steel cord parameters must be specified during procurement?
Specifying only “ST2500 belt, 1800 mm wide” is insufficient for engineering procurement. The purchaser must specify a complete set of carcass parameters:
- Cord Diameter & Pitch: Directly impacts belt flexibility, weight, and pulley size.
- Cord Lay & Construction: Cords must be arranged in alternating Left-hand and Right-hand Lang Lay (L/R Lay) to neutralize belt torsional tendencies and prevent tracking issues.
- Cord Rubber Adhesion & Pull-out Strength: Critical for ensuring force transfer between steel cords and the surrounding rubber matrix.
3. Does a higher ST rating always result in a better design?
No. Over-specifying belt strength creates a cascade of mechanical and financial disadvantages. Higher ST ratings require:
- Larger Pulley Diameters: Bending fatigue stress on thicker steel cords demands larger drive and return pulleys (e.g., ST1600 requires min. 1,000 mm pulleys, whereas ST2500 requires min. 1,250 mm).
- Increased Mass & Power Loss: Heavier belts increase moving mass, drive power consumption, and structural loading.
- Complex Splices & Tighter Take-Up Systems: Higher ST ratings necessitate multi-step vulcanized splices, increasing installation downtime.
The optimal engineering approach is to select the lowest ST rating that safely handles dynamic tensions while optimizing conveyor drive geometry and pulley sizing.
4. What is the realistic service life of a long-distance steel cord belt?
Engineering design must distinguish between Carcass Fatigue Life and Top Cover Wear Life:
- Steel Cord Carcass: Modern overland belts under continuous operation are commonly engineered around a 15 to 20-year carcass fatigue design life (e.g., the 12.589 km KPC OLC-2 project in Indonesia was designed with a 15-year baseline).
- Rubber Covers: Cover wear depends on material abrasiveness, drop height, loading frequency, and belt speed. Top cover re-buffing or cold-repair is often executed at 5 ~8 year intervals, while the internal carcass remains intact.
5. What real-world project illustrates optimized steel cord belt selection?
The KPC OLC-2 Overland Conveyor in Indonesia serves as a benchmark reference:
| Parameter | Project Specification |
| Conveying Center Distance | 12,589 m (Single Flight) |
| Throughput (Nominal / Peak) | 4,000 t/h / 4,500 t/h |
| Belt Speed | 8.45 m/s |
| Belt Rating & Width | ST2250, 1100 mm |
| Material Conveyed | Washed Coal |
| Design Life Assumption | 15 Years |
Engineering Insight: Despite a flight length exceeding 12.5 km and high throughput, the system was engineered with ST2250 rather than an extreme ST4000/ST5000 grade. This was achieved by optimizing drive positioning, low-rolling-resistance (LRR) cover compounds, and low idler friction coefficients (f ≤0.012).
6. Why is splice performance more critical than the belt’s nominal strength?
The vulcanized splice is the structural link transferring high dynamic tension along the entire belt loop. It is frequently the point of dynamic fatigue initiation.
- Splice Steps: Higher strength grades require multi-step splice geometry (1-Step for ST1000–ST2000; 2-Step or 3-Step for ST2500–ST4000; up to 4-Step for ST5400) to distribute shear stress evenly through the rubber interlayer.
- Dynamic Splice Efficiency (DIN 22110-3): Long-distance belts must be evaluated based on dynamic fatigue limit tests under cyclic stress. A single defect in cord alignment, rubber adhesion, or curing pressure can reduce fatigue strength, leading to catastrophic full-width failure.
7. When should a tear-resistant belt be specified instead of increasing the ST rating?
If the primary operational risk is longitudinal belt tearing caused by trapped tramp metal, sharp rocks, or excavator teeth: Increasing the ST rating (e.g., from ST2500 to ST4000) will NOT prevent longitudinal rips. Penetration occurs in the rubber gaps between parallel cords.
For high-impact or tear-prone environments, specify:
- Transverse Steel Cord Breakers: Steel or synthetic cords laid orthogonally above/below the main carcass to absorb puncture energy.
- Embedded Sensor Loops: RFID or inductive coil systems integrated into the belt, coupled with automated rip detection systems to instantly shut down drives upon penetration.
8. How do I match pulley diameters with steel cord belt ST ratings?
Pulley diameters must be calculated using fatigue stress limits under maximum cord bending. Recommended minimum drive pulley diameters per standard ISO 15236 / DIN 22101 categories (High Tension Duty – Group A) are listed below:
| Belt Strength Rating | Recommended Min. Drive Pulley Diameter (DA)* |
| ST1000 – ST1250 | 800 mm |
| ST1600 – ST2000 | 1,000 mm |
| ST2500 | 1,250 mm |
| ST3150 | 1,400 mm |
| ST4000 | 1,600 mm |
| ST4500 – ST5000 | 1,800 mm |
| ST5400 | 2,000 mm |
*For tail/take-up pulleys with lower dynamic wrap tension (Group B/C), diameters can be reduced by 1 step according to design codes.
9. How does high belt speed (>6m/s) affect belt selection?
Modern overland conveyors frequently operate at speeds of 6.0 ~10.0m/s. High belt speed shifts engineering priorities beyond static tensile calculations:
- Dynamic Wave Propagation: High speeds can excite fundamental transverse vibration harmonics between idler sets.
- Aerodynamic Drag & Power Dissipation: Air resistance on moving material and conveyor structure increases non-linearly with velocity.
- Material Impact Energy: Material degradation and loading cover wear scale quadratically with velocity differences at transfer chutes. High-speed belts require specialized impact-absorbing compounds and optimized troughing transitions.
10. What is the standard for modern condition monitoring of steel cord belts?
For long-distance conveyors, proactive condition monitoring replaces traditional calendar-based inspection with a multi-layered diagnostic system:
- Internal Carcass Inspection: Non-destructive Electromagnetic Inspection (EMI) scans 100% of internal steel cords to identify broken wires, cord corrosion, and splice displacement trending over time.
- Cover Surface Profiling: 3D laser scanners monitor cover wear thickness across the belt profile, allowing precise prediction of top cover service life.
- Rip Protection: Embedded sensor coils continually monitor for real-time longitudinal tearing.
Transitioning to predictive, condition-based inspection prevents catastrophic belt breakages and optimizes lifecycle maintenance costs.
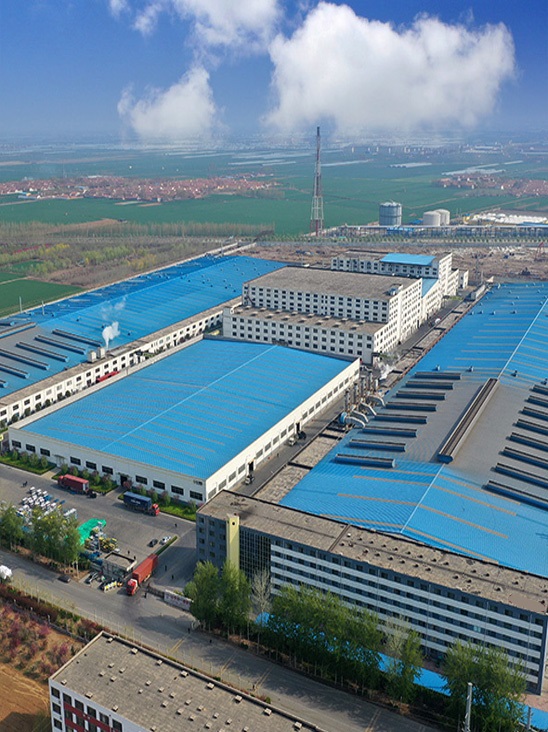
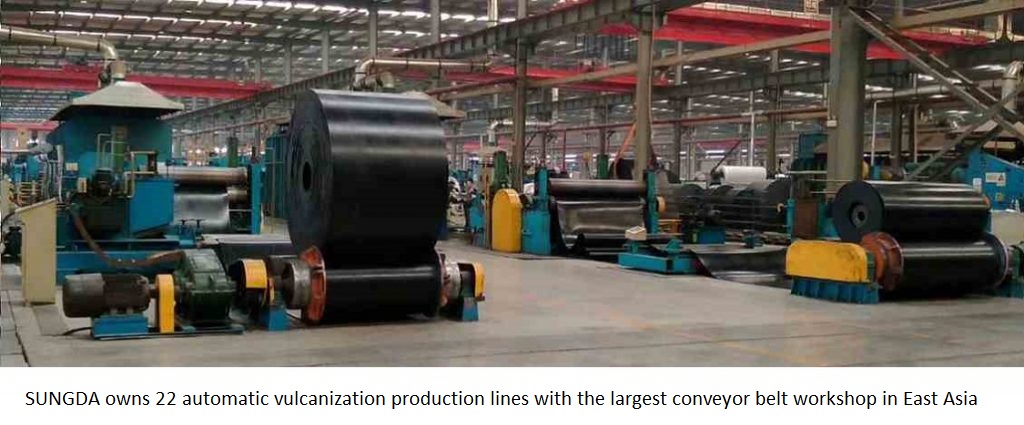
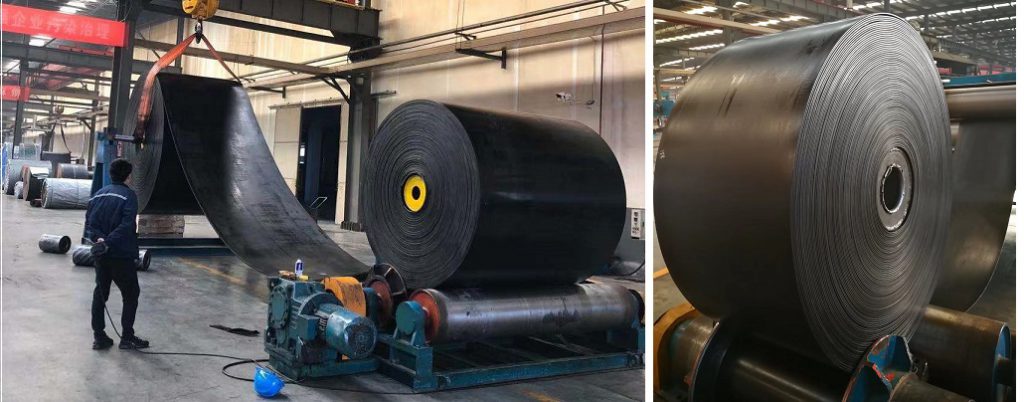
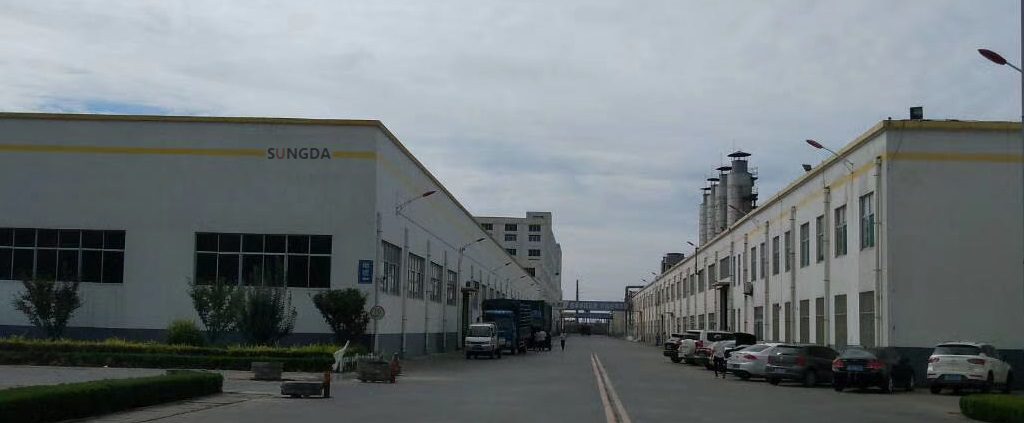
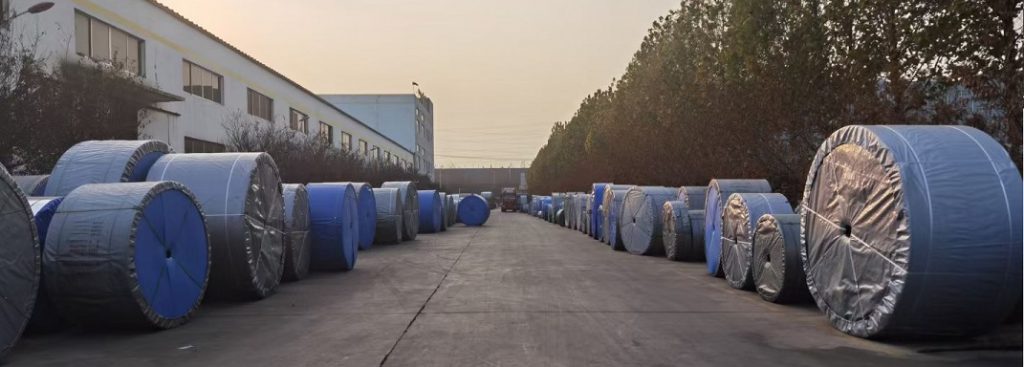
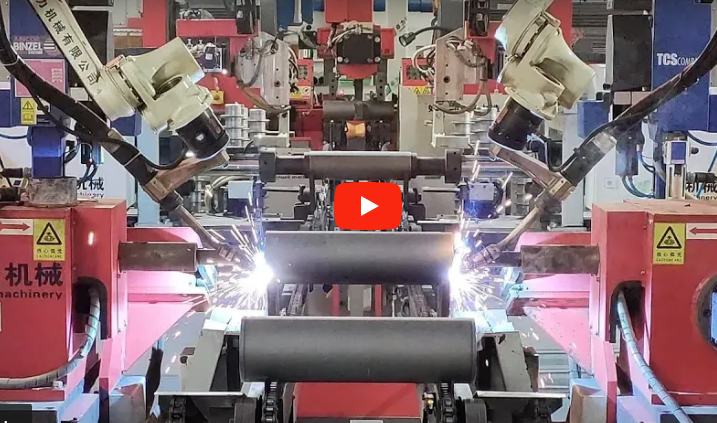
Sungda Conveyor Belt Vulcanization Workshops
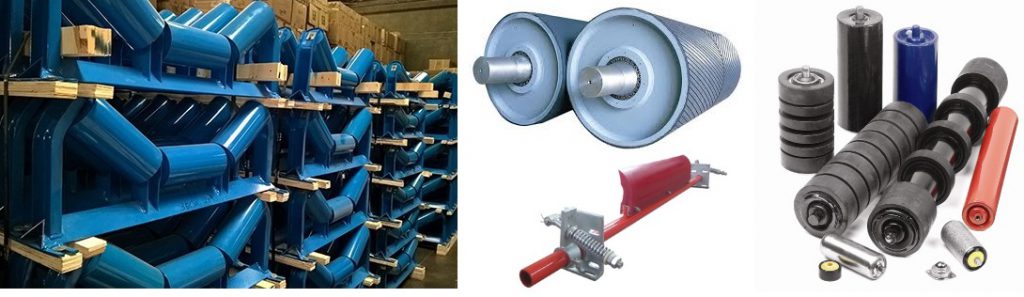
We also supply conveyor idlers, pulleys and conveyor brackets, please log on our brach company www.conveyoroller.com for more information.
Tags: Advantages and features of steel cord conveyor belts,applications of steel cord conveyor belts,Buying guide for steel cord conveyor belts,Common issues and troubleshooting for steel cord conveyor belts,Comparison of steel cord conveyor belts with textile conveyor belts,Customization options for steel cord conveyor belts,Industries that use steel cord conveyor belts,Innovations and advancements in steel cord conveyor belts,Installation and setup of steel cord conveyor belts,International standards and regulations for steel cord conveyor belts,Lifespan and durability of steel cord conveyor belts,Load capacity and weight-bearing capabilities of steel cord conveyor belts,long distance steel cord conveyor belt,Maintenance and care for steel cord conveyor belts,Manufacturers of steel cord conveyor belts,mining steel cord conveyor belt,PIW,Pricing and cost of steel cord conveyor belts,ST1000,ST1000 steel cord conveyor belt,ST1250 steel cord conveyor belt,ST1400,ST1600,ST1600 steel cord conveyor belt,ST2000 steel cord conveyor belt,ST2500 steel cord conveyor belt,ST3150 steel cord conveyor belt,ST630,ST630 steel cord conveyor belt,ST800,ST800 steel cord conveyor belt,Steel cord conveyor belt,Steel cord conveyor belt vs. other types of conveyor belts,steel mill,transverse reinforcing fabric,TRF,underground mining conveyor belt
Related Products
-
Material Composition of High-Quality Conveyor Belts (from ContiTech & Dunlop)
No. -
How to Chooe Right Steel Cord Conveyor Belt
No. -
What are the Basic Indicators that Determine the Quality of Conveyor Belts?
No. -
What Are the Key Properties of T1, T2, T3, T4 Heat-Resistant Conveyor Belts?
No. -
What’s “kg/cm²” in Conveyor Belt and How Convert it into other Units?
No. -
How to conduct conveyor belt troughing test
No. -
The Most Comprehensive National and Organizational Conveyor Belt Testing Standards
No. -
7 Common Causes of Conveyor Belt Tearing and What are the Preventive Measures?
No. -
What are the daily maintenance measures for steel cord conveyor belts?
No. -
What are the commonly used methods for non-destructive testing of steel cord conveyor belts
No.