


Fire Resistant Conveyor Belt(DIN-K)
Application Background:
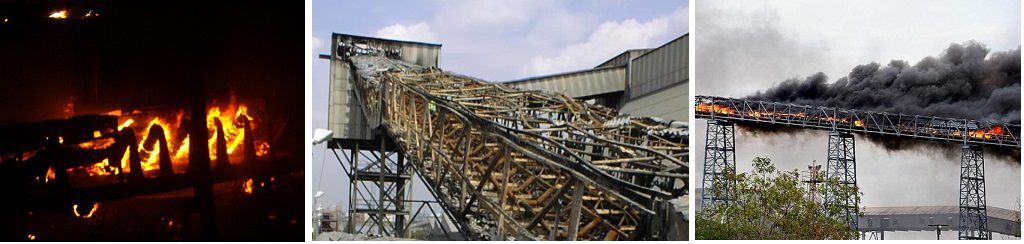
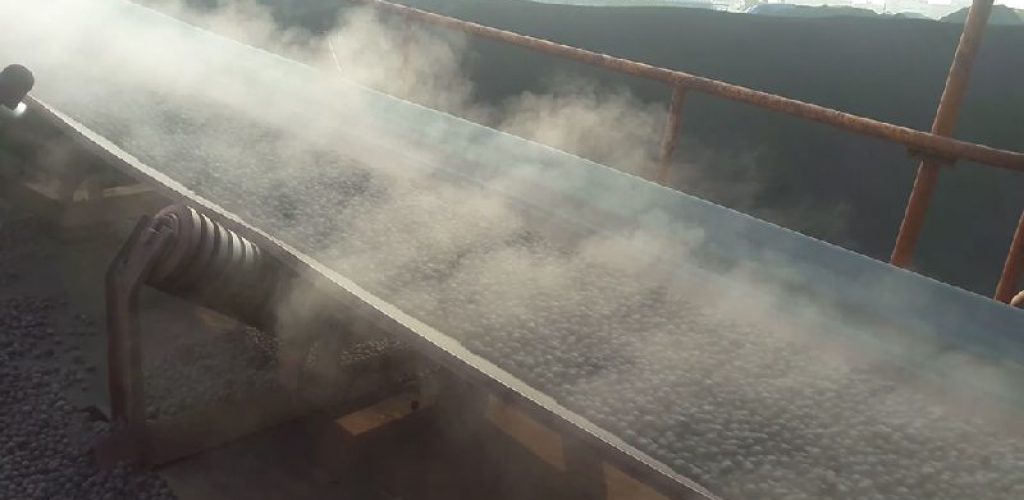
The use of fire-resistant (also called flame-resistant) conveyor belts (Standard:DIN-K/EN12882/JIS-K) in coal mines is conducive to reducing the incidence of both above ground and underground fires. The working environment of coal mines is relatively complicated, coal dust and gas are dangerous factors, and the coal mines being transported are also flammable substances, if electric sparks are generated during transportation, it is easy to cause fires. The use of fire-resistant conveyor belts for coal mines reduces the possibility of electrostatic sparks during coal transportation, and even if static sparks occur, the fire-resistant conveyor belts for coal mines have high flame resistance and maximize the flame spread time.
Currently, there are various flame-retardant conveyor belt standards around the world to ensure the safe use of conveyor belts, such as Germany’s DIN-K, Europe’s EN 12882 (general/above ground) and EN 14973 (underground), ISO 340, the USA’s MSHA 30, Japan’s JIS-K, and Australia’s AS 4606:2012. It is important to note that determining the specific flame-retardant level required for a particular application or environment is crucial. If you are unsure about the required fire resistance level, it is advisable to seek professional advice.
Fire Resistant Capability Test:
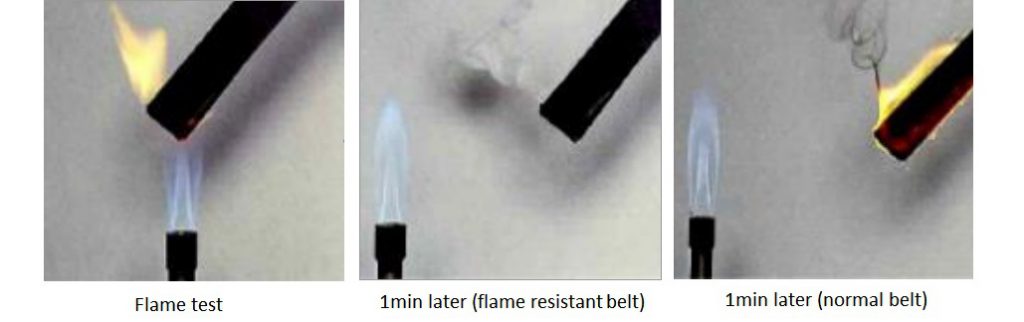
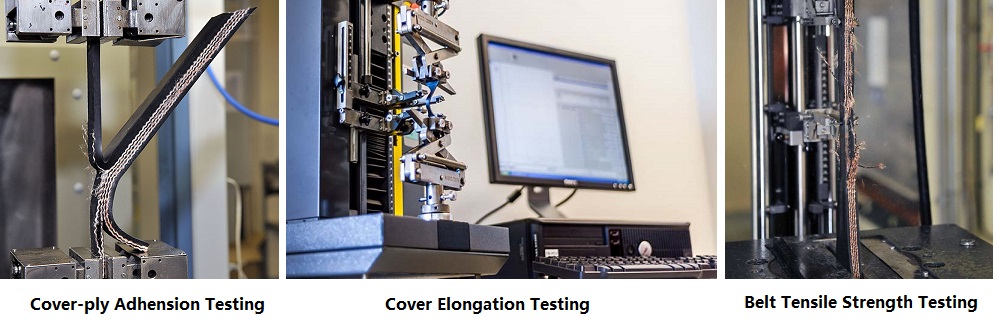
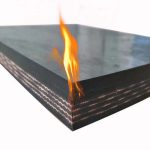
JIS/ISO/DIN tests involve exposing six individual samples of a belt to a naked flame, causing them to burn, the source of the flame is then removed and the combustion time (duration of flame) of the test piece is recorded, a current of air is then applied to the test piece for a specified time after the removal of the flame, the flame should not reignite. The time it takes for the belt sample to self-extinguish after the source of ignition (flame) has been removed is then measured. The duration of continued burning (visible flame) should be less than 15 sec. for each sample, with an absolute maximum cumulative duration of 45 sec.
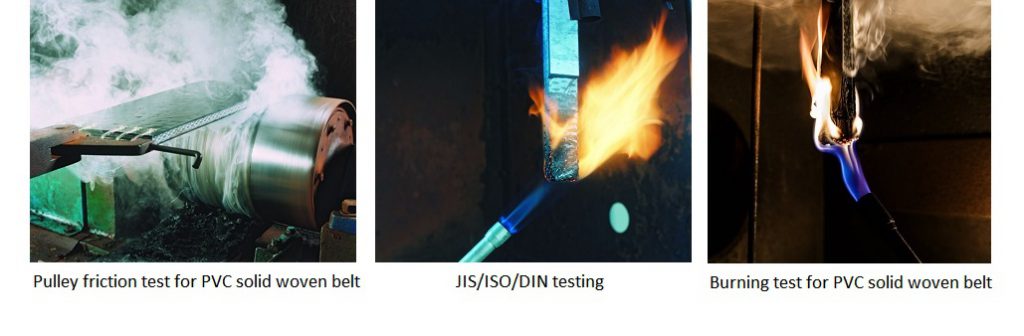
Pulley friction test is the single biggest difference in the safety classifications (standards) between belting used above ground and belting used underground. If certification is required, then these tests must be carried out by an independent test organization. The test standards demand that there should be no evidence of flame or glow during or after the test. This is only achievable by using a PVC belt because the thermoplastic melts/breaks before it reaches 325˚C, the SUNGDA maximum average is around 260 – 270˚C.
Fire resistant conveyor belt carcass type:
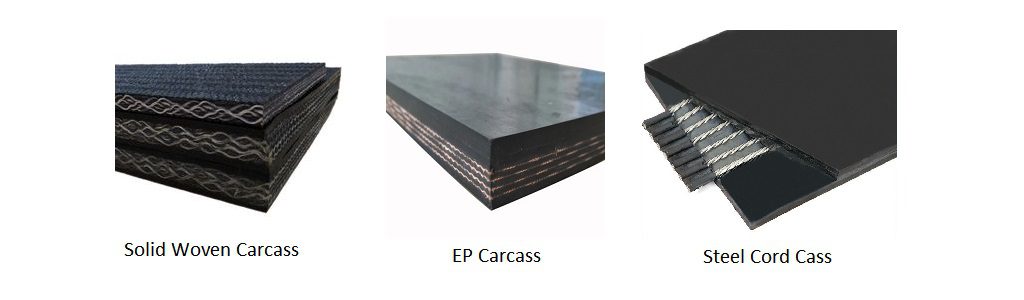
Solid woven carcass: This type of carcass woven by Polyester and Nylon filament, dipped through PVC and plasticized, with characteristics of high tensile strength, small elongation, non-peel off, light-body, no delamination, impact resistance, and tear-performance. Mainly applicable to the underground coal mine and other anti-static fireplaces
EP carcass: EP fabric includes polyester toward longitudinal (warp) and polyamide for latitude (weft), with lower longitudinal elongation, full resistance to mildew, moisture and rotting, good flexibility and trough ability. Suitable for middle and long-distance transportation of higher load and speed in the above-ground mining site.
Steel cord carcass: steel cord has super high tensile strength, good trough ability, high adhesion between rubber and steel cord, this type of fire-resistant belt is suitable for large span, long-distance transportation of materials.
When selecting flame-retardant conveyor belts, understanding the customer’s usage environment is crucial. Conveyor belts are used in a variety of settings, from dust-laden factory workshops to explosive environments like mines, as well as in complex outdoor and underground operations. Different scenarios impose different requirements on the flame-retardant properties of conveyor belts. Therefore, scientifically analyzing these environmental conditions, combined with the anti-static and flame-retardant properties of the conveyor belt, ensures safety and efficiency.
Currently, there are three main types of fire-resistant conveyor belts: fabric-layered fire-resistant conveyor belts, steel cord conveyor belts, and solid woven conveyor belts. Among the three types of fire-resistant conveyor belts used in coal mines, the fabric-layered conveyor belt is the most widely used, accounting for over 80% of the market share. It offers stronger flame retardancy while being lighter and more cost-effective.
Fire Resistant Test Internation Standards:

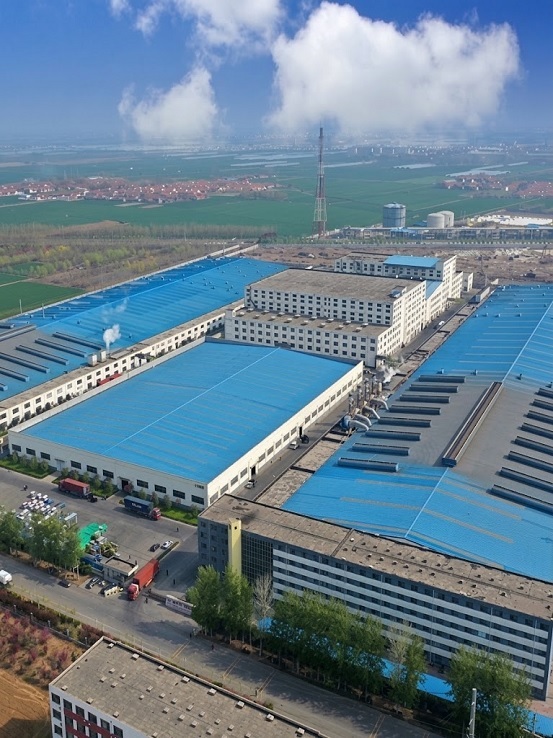
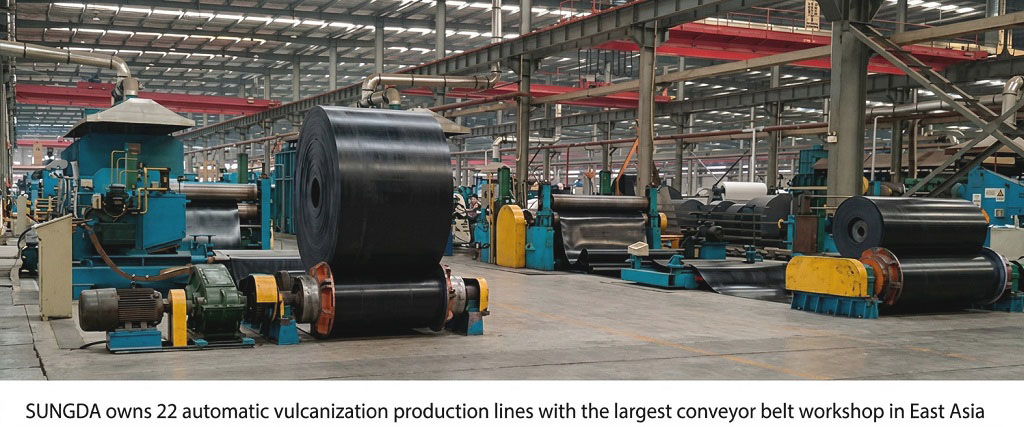
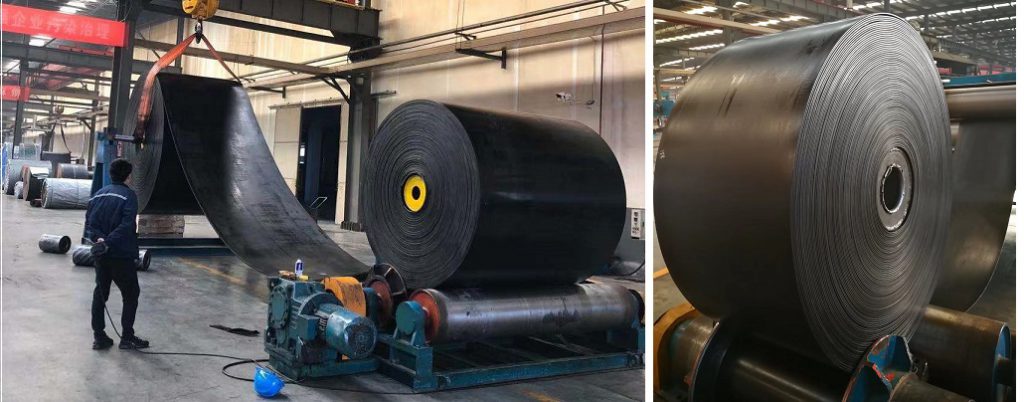
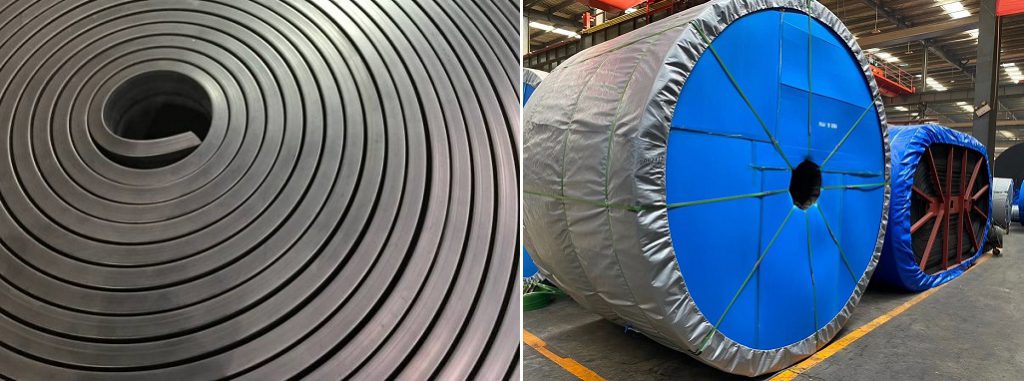
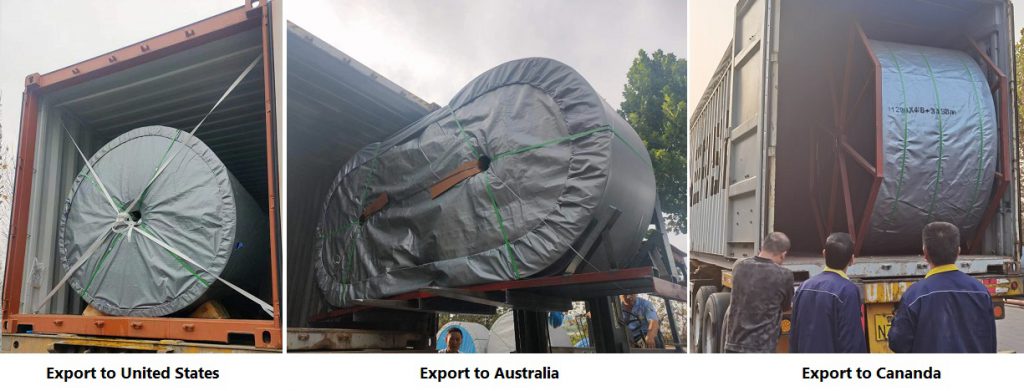
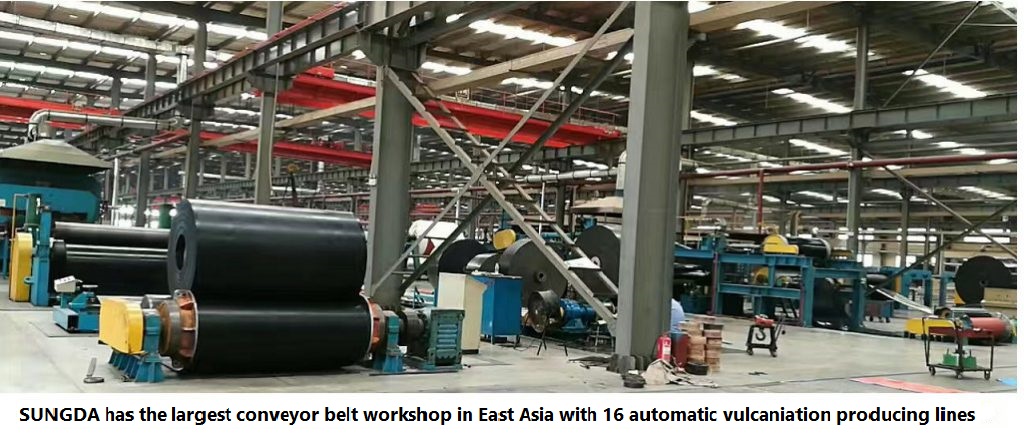
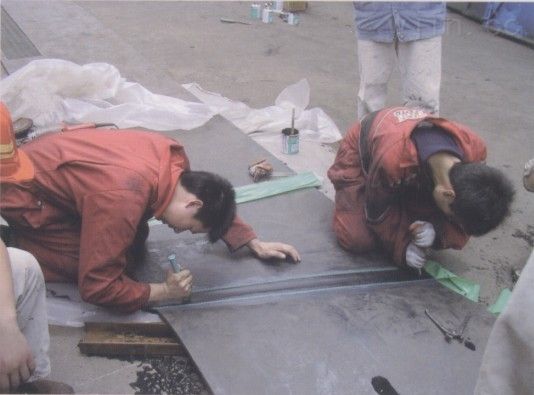
SUNGDA Conveyor Belt Vulcanization Workshops
10 Technical FAQs About Fire-Resistant Conveyor Belts for Underground & High-Hazard Conveying
1.What are the key international safety standards for Fire-Resistant (FR) conveyor belts, and how do they differ?
Selecting a fire-resistant conveyor belt requires strict adherence to regional and industrial safety mandates. Fire resistance is not a single property; it encompasses surface flammability (flame propagation), drum friction ignitability, and toxic smoke/gas emission limits.
The primary global testing standards dictate where and how an FR belt can be deployed:
| Standard / Certification | Geographical / Industry Domain | Primary Test Methods Required | Typical Applications |
|---|---|---|---|
| ISO 340 / EN 12882 | Global / European General Industry | ISO 340 Laboratory Burner Test & ISO 284 Electrical Conductivity | Aboveground hazardous sites, grain handling, power plants |
| DIN 22100 / EN 14973 | Europe / Germany Underground Mining | Propane Gallery Test (Class C/K/S), Drum Friction Test | Underground hard-rock and coal mining |
| MSHA Part 14 / Part 18 | USA Underground Mining (MSHA Approved) | MSHA Flame Test Chamber & Gallery Friction Test | US underground coal mines, dusty enclosed spaces |
| CAN/CSA M422 | Canada Mining & Industrial | Flame Test (Class A/B/C) & Surface Friction Igneability | Underground Canadian mining, high-risk processing plants |
| AS 1332 / AS 1334 | Australia Underground & Surface Mining | Laboratory Burner, Friction Drum, & Oxygen Index (OI ≥ 30%) | Australian coal mines, export ports |
Engineering Rule: For underground coal mining or enclosed gallery conveying, specifying a belt that only meets ISO 340 is insufficient. Underground applications mandatorily require full-scale Gallery Flame Tests (e.g., EN 12882 Class 4 or 5 / MSHA Title 30) to simulate real tunnel ventilation and heat feedback.
2.How does the ISO 340 Flame Retardancy Test work, and what defines a “pass”?
The ISO 340 Laboratory Burner Test evaluates the self-extinguishing capability of a conveyor belt sample after direct exposure to a high-temperature naked flame.
Testing Methodology: A test piece (210 mm × 25 mm) cut from the full thickness of the belt (including covers and carcass) is suspended vertically inside a test chamber. A standardized gas burner flame (1000°C ± 20°C) is applied to the bottom edge of the sample for 45 seconds under still air conditions, then withdrawn. The burner is applied a second time for 45 seconds to a new sample under forced airflow (1.5 m/s) to simulate tunnel ventilation.
Pass Criteria: The duration of flame or glowing combustion after removing the burner must not exceed 45 seconds for any individual test piece. The total duration of flame or glowing for a set of 6 test pieces must not exceed 120 seconds. Re-ignition of the sample must not occur when air currents are applied.
3.What is the Drum Friction Test, and why is it critical for belt safety?
A major cause of underground conveyor fires is stalled-belt friction. If a conveyor belt slips over a rotating drive pulley due to jam-up or low tension, severe mechanical friction generates intense localized heat. If the rubber compound is not formulated correctly, this friction can ignite the belt and cause catastrophic tunnel fires.
The Drum Friction Test (ISO 323 / EN 1554): A full-thickness belt sample is wrapped around a stationary steel drum driven at a constant surface speed (typically 2 m/s) under high static tension (750 N ~ 1200 N). The test runs continuously for 60 minutes or until the belt breaks.
Critical Safety Thresholds: Maximum Drum Temperature: The surface temperature of the steel drum must not exceed 325°C ~ 400°C (depending on standard tier). No Glow or Flame: The belt sample must not exhibit any flame, glowing embers, or sparks during or after the test period.
Formulating cover compounds with specialized fire-retardant additives absorbs frictional energy through endothermic reactions, keeping drum temperatures well below the ignition point of coal dust or methane gas.
4.What chemical compounds are used to manufacture Fire-Resistant conveyor belts?
Achieving fire-retardant properties without sacrificing mechanical abrasion resistance requires specialized elastomer formulation and additive engineering:
PVC / PVG Compounds (Solid Woven Belts): Polyvinyl Chloride (PVC) naturally contains chlorine, an inherent fire suppressant. PVG (PVC covered with an outer nitrile/SBR rubber layer) blends high fire safety with improved friction grip and slope performance. Highly popular in underground coal mining.
Neoprene / Chloroprene (CR): Chloroprene rubber features halogen-containing molecules that release flame-extinguishing radical gas when heated. CR offers superior oil resistance, mechanical toughness, and fire safety, though at a higher material cost.
EPDM / SBR with FR Fillers: For standard rubber-covered fabric (EP) or steel cord belts, synthetic elastomers (SBR/EPDM) are heavily loaded with functional fire-retardant additives: Aluminum Trihydrate (ATH) / Magnesium Hydroxide (MDH): Releases water vapor endothermically when heated, cooling the flame zone and diluting combustible gases. Antimony Trioxide (Sb₂O₃): Acts synergistically with halogenated polymers to choke gas-phase flame propagation. Zinc Borate: Promotes the formation of a protective insulating char layer over the carcass.
5.Why is Electrical Conductivity (ISO 284 / Anti-Static) mandatory on Fire-Resistant belts?
Fire resistance alone is insufficient in explosive environments like coal mines, grain silos, or chemical plants. As a conveyor belt runs over idlers and pulleys, continuous surface friction generates static electricity charges up to tens of thousands of volts.
If the belt surface is non-conductive, this static charge accumulates until it discharges via an high-energy electrostatic spark, which can instantly ignite airborne coal dust, grain dust, or methane gas (CH₄).
ISO 284 Anti-Static Specification: To prevent charge accumulation, anti-static carbon black or conductive agents are mixed into the rubber compounds.
Electrical Resistance (R) ≤ 3 × 10⁸ Ω (300 MΩ)
Safety Requirement: Standard ISO 284 testing requires the surface electrical resistance measured between two electrodes placed on the belt cover to not exceed 300 MΩ. In coal mines, stricter local limits often mandate R ≤ 10⁶ Ω (1 MΩ).
6.Solid Woven (PVC/PVG) vs. Multi-Ply Fabric (EP FR) vs. Steel Cord (ST FR): Which carcass structure should be selected?
The internal carcass selection governs the mechanical capacity and structural duty of the fire-resistant belt:
| Carcass Type | Construction Feature | Flame Performance | Mechanical Best Suitability |
|---|---|---|---|
| Solid Woven (PVC / PVG) | Single-ply heavy woven textile impregnated with PVC paste | Highest: Fully impregnated carcass leaves no internal air pockets for combustion | Underground coal mining, short to medium center distances, impact-prone loading |
| Multi-Ply Fabric (EP FR / NN FR) | Multiple rubber-insulated synthetic plies with FR covers | Moderate: Requires FR rubber skim coats between plies to prevent internal burning | Aboveground processing, power plants, grain elevators, aggregate plants |
| Steel Cord (ST FR) | Longitudinal steel cords embedded in FR rubber matrix | High: Inorganic steel core does not burn; low organic mass fraction | Long-distance overland coal transport, deep-shaft mine slopes, high-tonnage lines |
Engineering Rule: For underground coal mining, Solid Woven (PVG) belts are widely preferred over multi-ply EP belts because multi-ply construction can suffer internal ply delamination, allowing trapped air and coal dust to sustain hidden smoldering combustion inside the carcass.
7.Does a Fire-Resistant belt mean the belt is Heat-Resistant (HR), and vice versa?
No. Fire Resistance (FR) and Heat Resistance (HR) are fundamentally different material properties.
Fire-Resistant (FR) Belts: Engineered to self-extinguish when direct flame or ignition sources are removed and to prevent static spark generation. FR belts are designed for safety compliance in hazardous atmospheres, not for conveying hot materials.
Heat-Resistant (HR) Belts: Formulated to resist thermo-oxidative degradation, hardening, and cracking caused by continuous contact with hot materials (120°C ~ 400°C, like cement clinker or sinter). HR compounds may burn readily if ignited by an open flame.
Dual-Rated Belts (FR-HR Grade): When conveying hot materials in a fire-hazard environment (e.g., hot coal ash in power plants, or hot sinter ore in enclosed galleries), you must specify a Combined Fire-Resistant AND Heat-Resistant (FR-HR / ISO 15236 FR-T) Grade belt formulated with specialized EPDM/CR blends and FR additives.
8.What causes smoke density and toxicity concerns, and how are they tested?
In underground mine fires or enclosed gallery blazes, toxic gas inhalation and zero-visibility smoke represent a greater threat to life than direct flame exposure.
Standard FR rubber formulations using brominated halogens can release toxic hydrogen chloride (HCl) or hydrogen bromide (HBr) fumes during combustion.
Modern Low-Smoke Halogen-Free (LSHF / EN 14973) Requirements: Advanced tunnel and underground specifications mandate strict smoke and toxicity limits: Smoke Density Testing (ISO 5659-2 / EN 13501-1): Measures light attenuation through smoke generated inside a sealed chamber. The Specific Optical Density (Dₛ) must stay below strict limits to allow evacuation visibility. Toxicity Index (EN 17084 / NES 713): Analyzes off-gassing for dangerous concentrations of Carbon Monoxide (CO), Hydrogen Cyanide (HCN), Sulfur Dioxide (SO₂), and Nitrogen Oxides (NOₓ).
Procurement Tip: When procuring belts for underground metro projects, utility tunnels, or enclosed grain galleries, specify Halogen-Free Flame Retardant (HFFR) compounds utilizing MDH/ATH chemistries to ensure non-toxic smoke during emergency fires.
9.How do FR rubber compounds affect splice design and field vulcanization?
Because fire-resistant rubber cover stock and tie gum are heavily loaded with non-combustible fillers (like ATH, zinc borate, or antimony), their rheological flow and cross-linking characteristics differ significantly from standard SBR compounds:
Slightly Lower Adhesion Strength: FR additives can reduce polymer-to-fabric peel strength. Splicing requires specialized FR tie-gum skim sheets and specific adhesive cements matching the parent compound. Tighter Curing Parameters: Field hot vulcanization requires precise temperature control (±5°C) and longer hold times to ensure full cross-linking of the flame-retardant matrix without thermal scorching. Splice Fire Integrity: The vulcanized joint area must maintain the exact same ISO 340 flame-retardant and ISO 284 anti-static ratings as the base belt loop. Standard un-rated repair patches must never be used on an FR belt.
10.What routine maintenance and condition monitoring standards apply to FR conveyor belts?
Maintaining the safety certification of a fire-resistant belt system requires monitoring both physical belt integrity and surrounding conveyor mechanics:
Surface Resistivity Testing (ISO 284 Checks): Periodically measure electrical resistance across the belt top cover using a megohmmeter. Dust buildup, oil contamination, or cover wear can raise electrical resistance beyond the 300 MΩ threshold, re-introducing electrostatic spark risks. Carcass Exposure & Fraying Checks: Inspect belt edges for frayed fabric plies or exposed steel cords. Frayed synthetic fibers act as wicks for coal dust and oil, increasing flammability risks. Idler Roller & Skirt Rubber Monitoring: Ensure that skirt rubber seals and scraper blades are made of certified FR anti-static materials. A seized idler roller or non-FR rubber skirt rubbing against the moving belt cover can generate localized frictional heat capable of triggering ignition. Cleanliness & Dust Suppression: Regularly wash down accumulated coal or grain dust from the return strand and structure. Combustible dust layers sitting on an FR belt negate the belt’s self-extinguishing properties during a fire event.
Comparison of RMA and DIN Standard for Conveyor Belts
The Top 5 Rubber Conveyor Belt Manufactures in China 2026(with website & contact info)
What is the difference between PSI and Mpa in conveyor belts and how to convert them to each other?
EP Conveyor Belt Layer is the More, the Better?
Tags: Anti-static properties of fire resistance conveyor belts,Applications and industries of fire resistance conveyor belts,AS 4606:2012,Case studies and successful applications of fire resistance conveyor belts,Chemical corrosion resistance of fire resistance conveyor belts,Comparison between fire resistance conveyor belts and other types,Design and manufacturing standards for fire resistance conveyor belts,DIN-K,Emergency response measures for fire incidents involving conveyor belts,EN 12882,EN 14973,Environmental characteristics and sustainability of fire resistance conveyor belts,Fire resistance grades and certifications for conveyor belts,Fire resistance performance testing standards for conveyor belts,fire resistant conveyor belt,fire retardant conveyor belt,Flame resistant conveyor belt,Flame retardant conveyor belt,FR conveyor belt,Heat stability and high-temperature resistance of fire resistance conveyor belts,Importance and role of fire resistance conveyor belts,Industry standards and regulations for fire resistance conveyor belts,Installation and maintenance tips for fire resistance conveyor belts,JIS-K,Lifespan and durability of fire resistance conveyor belts,Materials and construction of fire resistance conveyor belts,MSHA 30,Pricing and costs of fire resistance conveyor belts,PVC,PVG,Research and innovation trends in fire resistance conveyor belts,Selection and buying guide for fire resistance conveyor belts,Suitable environments and conditions for fire resistance conveyor belts,underground mining fire resistance conveyor belt
Related Products
-
DIN-X,DIN-W,DIN-Y and DIN-Z Rubber Conveyor Belt –SUNGDA
No. -
Steel Cord Conveyor Belt
No. -
The Most Comprehensive National and Organizational Conveyor Belt Testing Standards
No. -
What is the Difference between Heat-Resistant Conveyor belts and Fire-resistant conveyor belts?
No. -
How to make the heat-resistant conveyor belt can reach the level of 800 °C?
No. -
The King of High Temperature Resistant conveyor belt— EPDM Conveyor Belt
No. -
How the conveyor belt is fireproof and anti-static
No. -
Ways to prevent off tracking of the integral carcass flame resistant conveyor belt
No. -
Various connection methods of flame resistant conveyor belt
No. -
Development trend of rubber flame resistant conveyor belt
No.